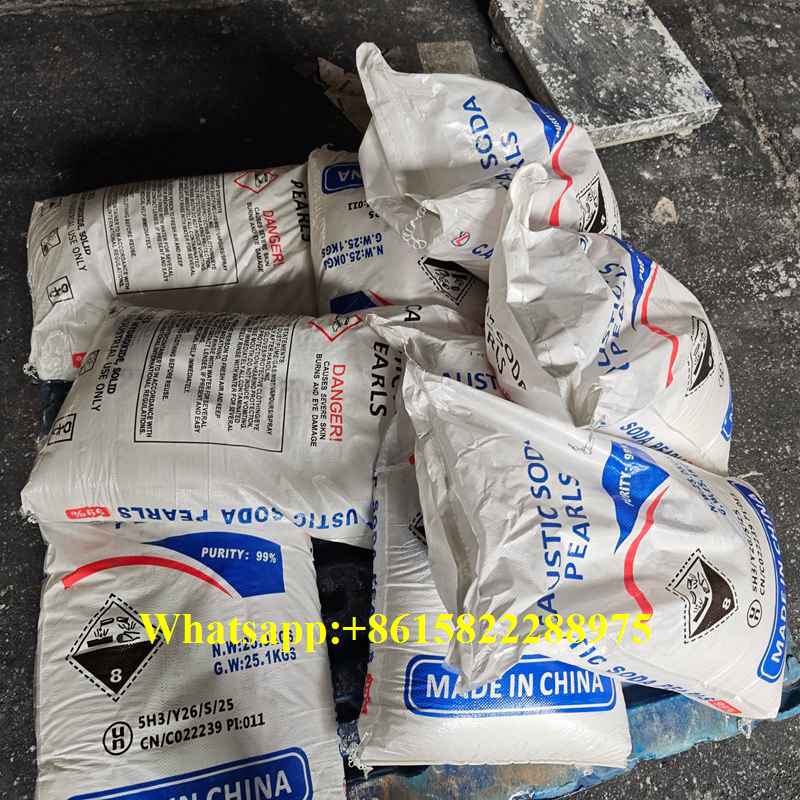
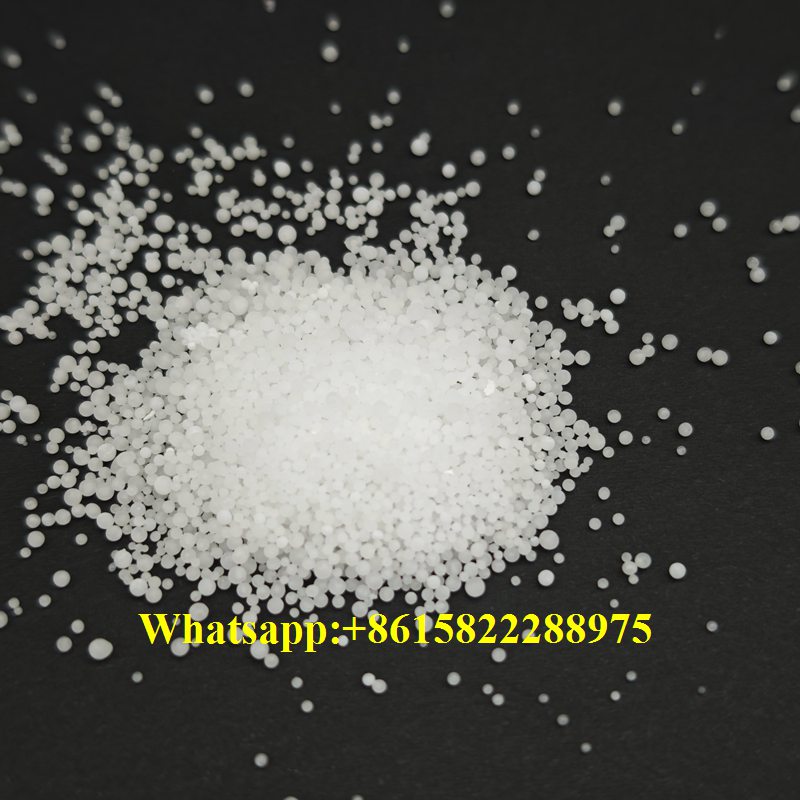
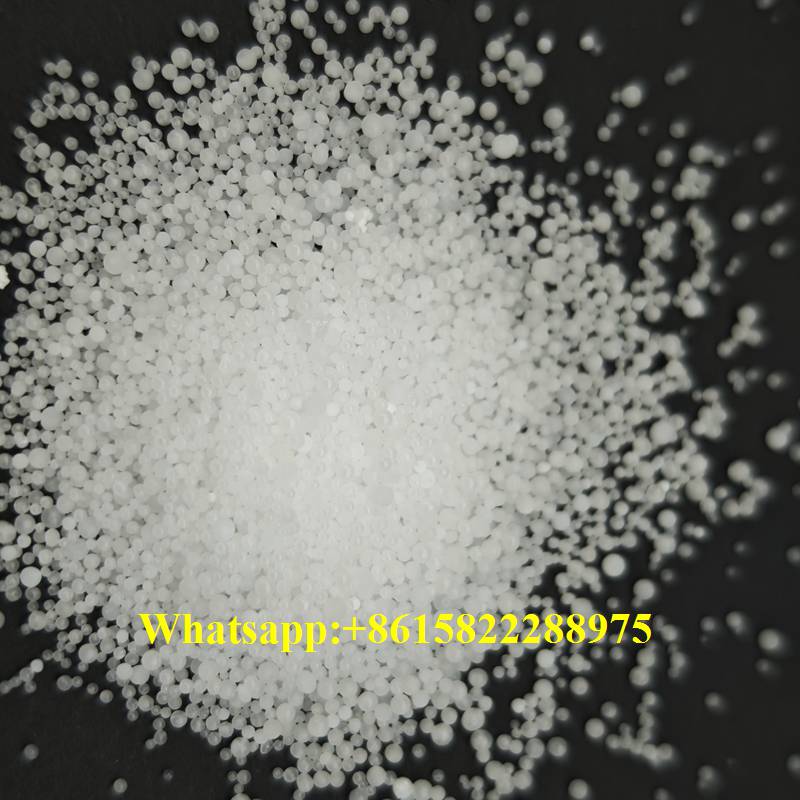
For multinational processing corporations and industrial distributors, partnering with competent bulk chemical suppliers is essential for maintaining uninterrupted plant operations and controlling procurement risks. High-volume raw material sourcing requires far more than basic manufacturing; it demands robust maritime logistics, dangerous goods (DG) regulatory compliance, and consistent product quality at scale. As an established primary producer and global export partner, our enterprise bridges heavy industrial synthesis with seamless ocean transportation to deliver primary alkaline reagents worldwide.
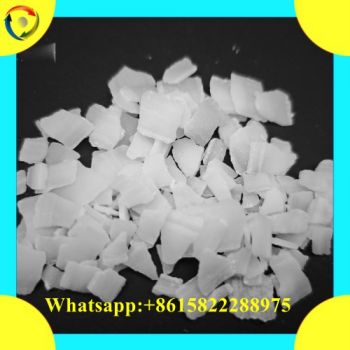
The distinction between standard trading entities and premier bulk chemical suppliers lies in integrated production and shipping infrastructure. Operating high-capacity ion-exchange membrane chlor-alkali complexes, our facilities generate industrial-grade sodium hydroxide ($\text{NaOH} \ge 99\%$) continuously, supporting multi-thousand-ton contractual commitments.
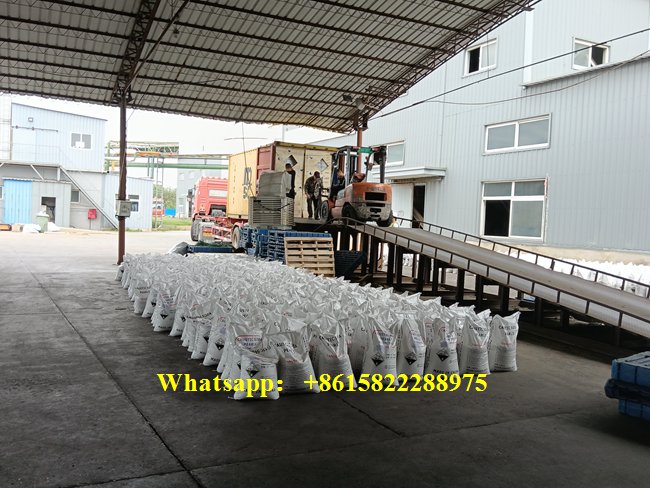
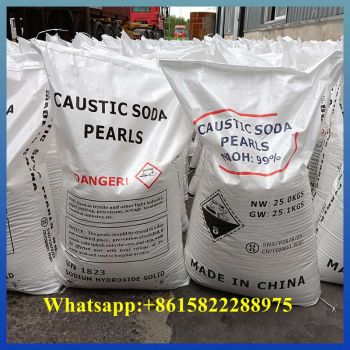
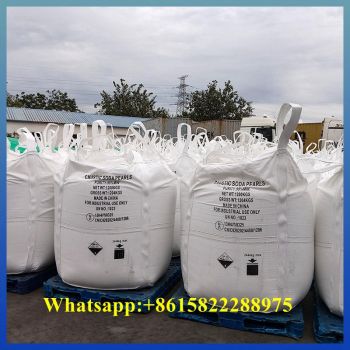
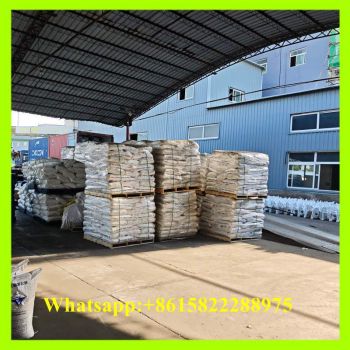
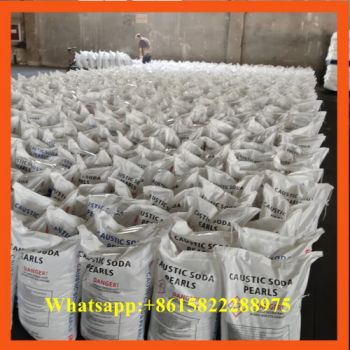
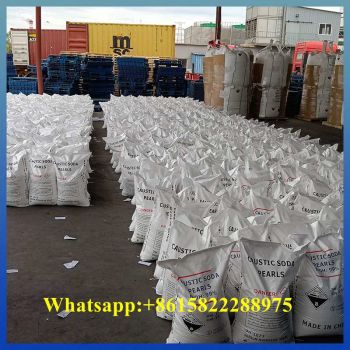
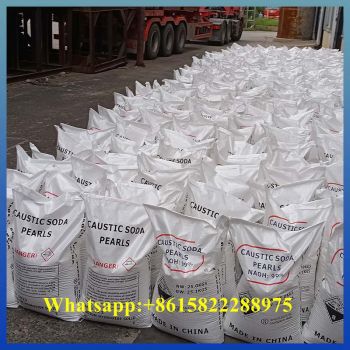
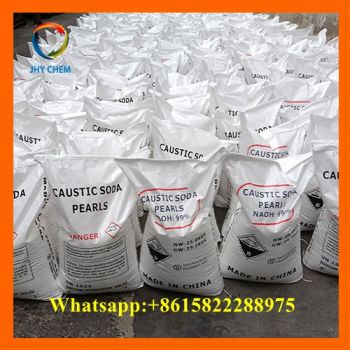
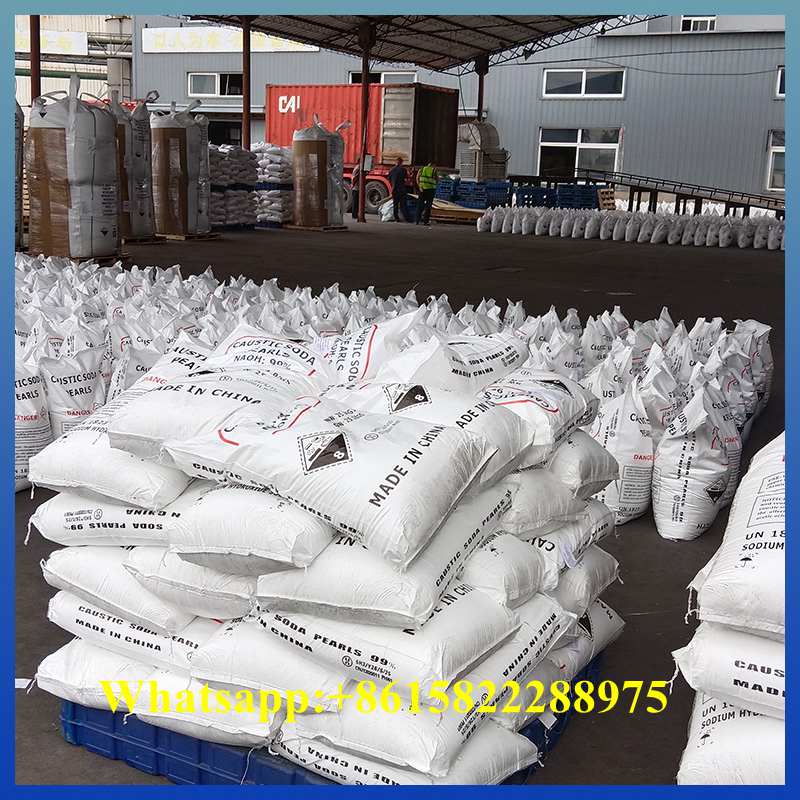
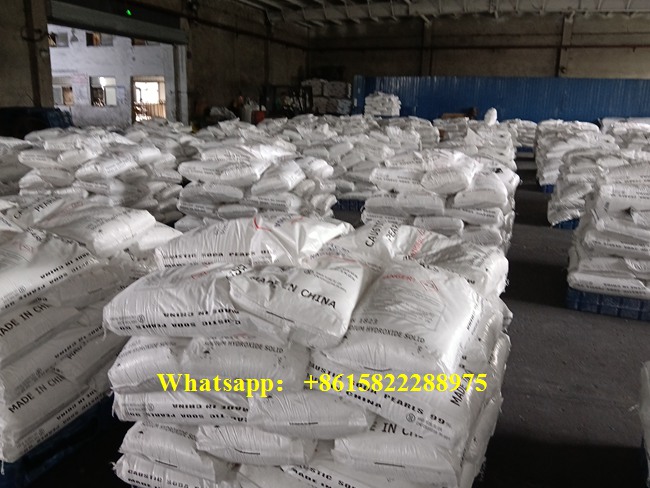
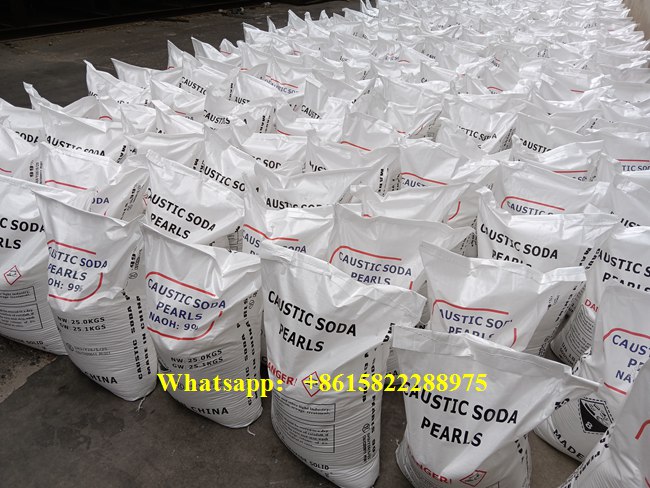
Managing high-volume chemical shipments requires advanced handling equipment to preserve compound integrity during long-distance transoceanic transit. From automated bag-filling stations to robotic palletization, our export halls prepare solid alkaline cargo for containerized and breakbulk vessel transport.
Every dispatch is engineered to prevent moisture ingress, reduce dust formation during discharge, and resist mechanical stress caused by maritime cargo handling across international ocean routes:
1. Strategic Proximity to Deep-Water Ports: Situated just 15 kilometers from Tianjin Port, our chemical production complex ensures rapid inland transit, eliminating port congestion delays and minimizing domestic freight overheads.
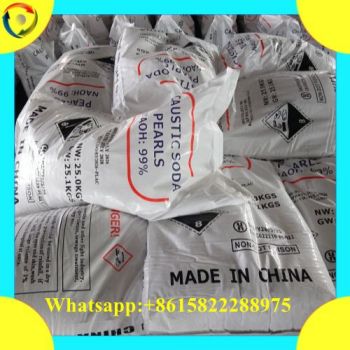
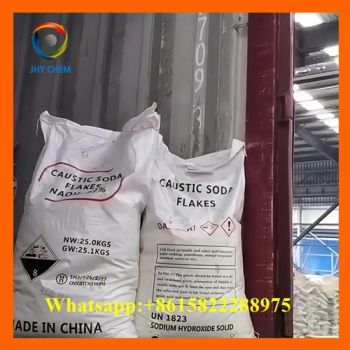
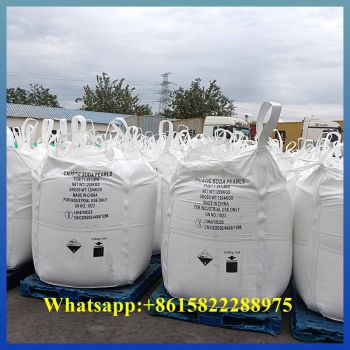
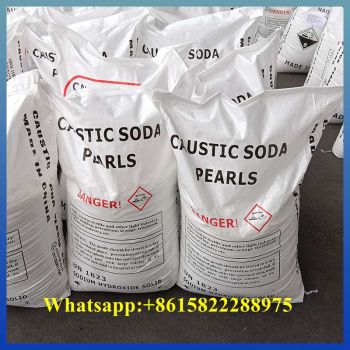
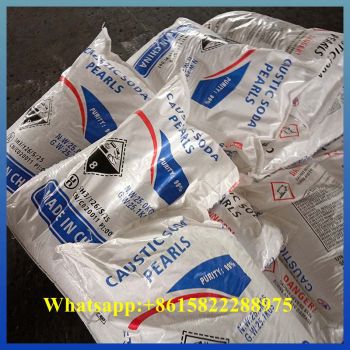
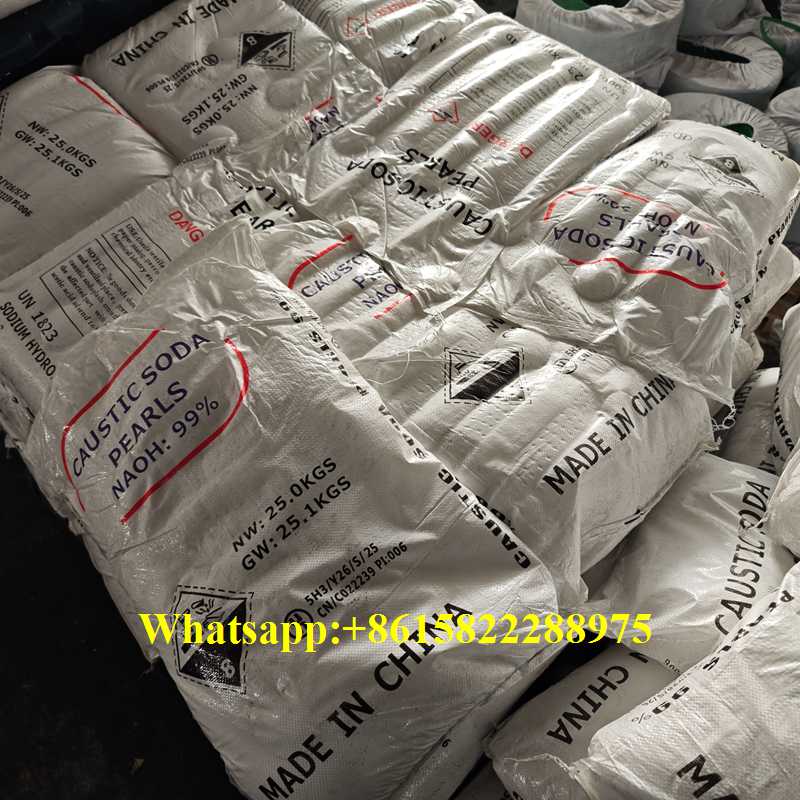
2. Flexible Packaging Solutions: We offer heavy-duty 25kg PP woven bags with heat-sealed PE inner liners, 1000kg Jumbo Bags for automated plant hoppers, and neutral OEM packaging for regional distributors.
3. Continuous Annual Output: With an annual chlor-alkali capacity of 120,000 metric tons, we guarantee stable cargo allocations without spot market supply disruptions.
Large-scale supply of high-purity solid sodium hydroxide underpins critical processing workflows across major industrial sectors worldwide:
● Alumina Refining (Bayer Process): Continuous high-tonnage supply of strong alkali required for bauxite digestion and alumina extraction in aluminum smelting complexes.
● Chemical Synthesis and Detergent Manufacture: Essential bulk neutralizing agent and saponification base for large-scale surfactant, liquid cleaning, and industrial soap production.
● Municipal and Industrial Water Treatment: Bulk alkalinity adjustment for large-scale wastewater neutralization, heavy metal precipitation, and municipal water purification.
● Pulp and Paper Kraft Processing: Scalable supply of pure alkali for wood chip cooking, continuous delignification, and multi-stage bleaching systems.
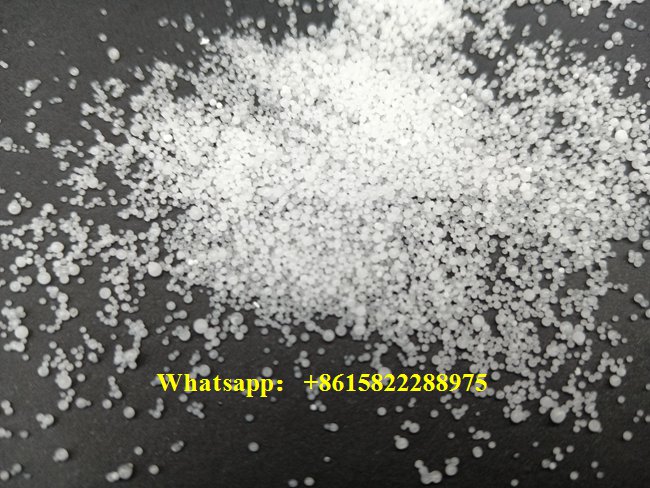
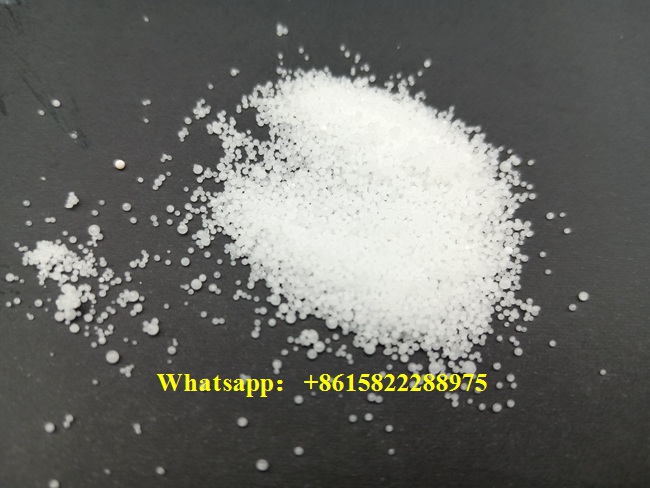
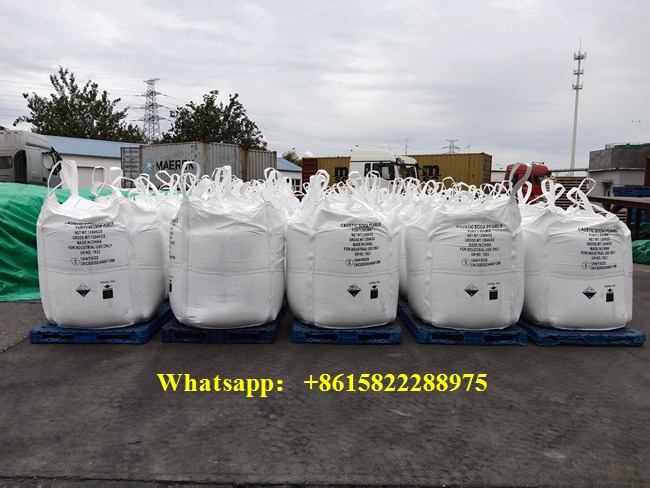
Sodium hydroxide in solid forms is classified as a Class 8 corrosive substance (UN 1823). Exporting large volumes requires strict adherence to international maritime dangerous goods (IMDG) standards. Every containerized shipment is backed by UN-certified packaging, a lot-specific Certificate of Analysis (COA), and GHS-compliant Safety Data Sheets (SDS).
Furthermore, our export documentation department easily manages port-specific compliance requirements across Africa, Latin America, and Europe, including tracking waivers (ECTN, BSC, FERI) and REACH compliance support. Contact our international trade team today to request custom wholesale quotations, review technical datasheets, or schedule full container load (FCL) shipments.
Tel:+86-22-66863746
Fax:+86-22-66863746 ext. 608
Mobile Phone:
+86-15822288975(WhatsApp)
E-mail: causticsoda@jiahengyuanchem.com
Add:NO.1023, 10F, BLDG B, JUNJING SQUARE, HANGYUN 1ST ROAD, TEDA, TIANJIN, CHINA