For industrial manufacturers, soap producers, water treatment plants, and chemical distributors across Africa, maintaining an uninterrupted and cost-effective caustic soda supply is the absolute backbone of profitable operations. Too often, regional procurement teams face severe hurdles: unpredictable price fluctuations from local traders, inconsistent product purity, and devastating moisture damage caused by inadequate packaging during long ocean voyages. At our advanced chemical manufacturing complex, we eliminate these systemic supply chain vulnerabilities by offering direct factory partnerships designed specifically to protect your profit margins and production schedules.
By cutting out costly middlemen, your enterprise gains immediate access to premium-grade sodium hydroxide (NaOH 99.0% minimum) backed by certified batch consistency and aggressive volume pricing. Whether you operate large-scale textile mills, gold extraction plants, or municipal purification facilities, our robust manufacturing capacity ensures your production lines never experience unexpected downtime due to material shortages.

Every batch of our alkali product is synthesized via state-of-the-art membrane cell electrolysis, yielding exceptional chemical clarity and minimal trace impurities. To accommodate diverse plant handling systems and automated dosing equipment, we provide three specialized commercial grades tailored for industrial excellence:
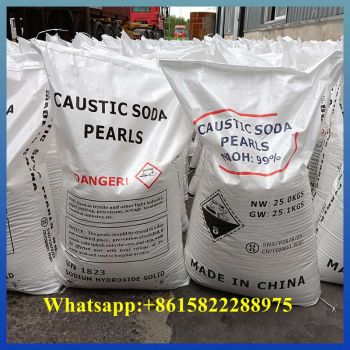
● High-Purity Caustic Soda Pearls: Engineered with uniform spherical geometry (0.8mm to 1.2mm), offering exceptional free-flowing performance, minimal dust generation, and precise volumetric feeding for automated industrial batching.
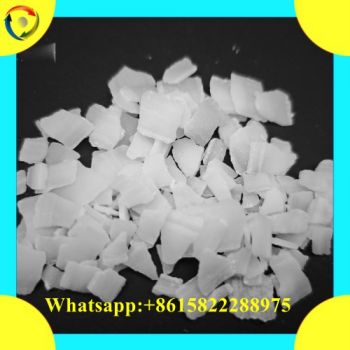
● Industrial Flakes (98% & 99%): Featuring a thin laminar crystalline structure designed for rapid, exothermic dissolution in aqueous solutions, perfect for heavy-duty degreasing and soap saponification.
● Concentrated Liquid Solutions (50% NaOH): Delivered in bulk ISO tankers or dedicated containers, providing instant plug-and-play capability for continuous industrial manufacturing lines.


Our high-reactivity sodium hydroxide delivers exceptional performance across the continent's most demanding economic sectors:
1. Soap and Detergent Manufacturing: Accelerates complete saponification of palm and vegetable oils, producing hard, bright, and highly active commercial cleaning bars.
2. Water Treatment and Sanitation: Neutralizes aggressive acidic effluents and precipitates toxic heavy metals in municipal and industrial wastewater systems.
3. Mining and Metallurgical Processing: Serves as a vital lixiviant and pH regulator in gold cyanide leaching and bauxite refining operations.
4. Textile Mercerization and Paper Pulp: Enhances cotton fiber dye absorption and supports efficient Kraft pulping and paper recycling.
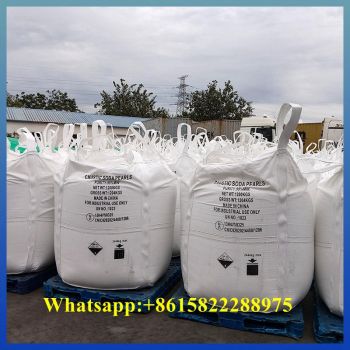
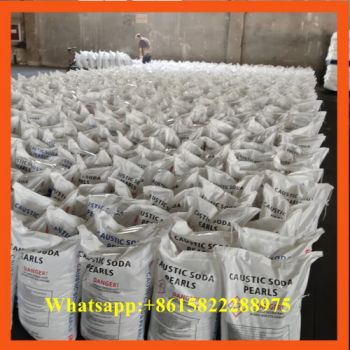
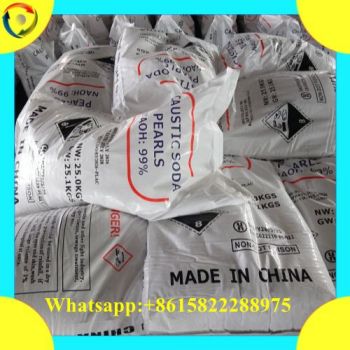
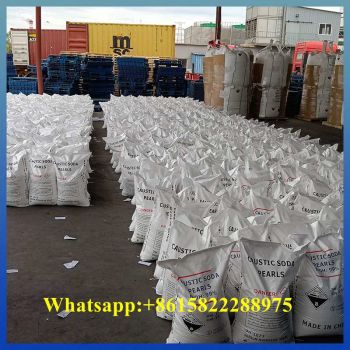
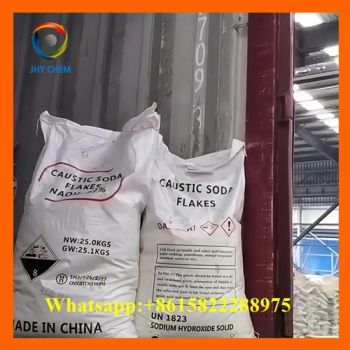
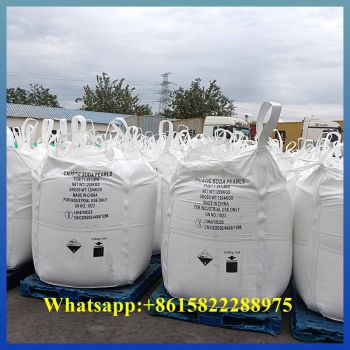
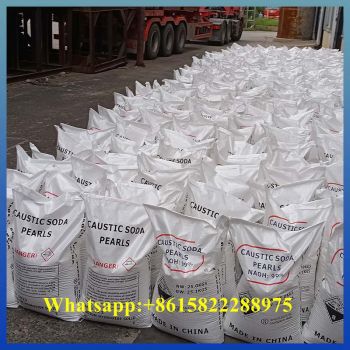
Shipping alkali chemicals across oceans and through tropical humid zones requires uncompromising packaging standards. To guarantee your order arrives in pristine, free-flowing condition, we utilize heavy-duty 25kg multi-layer polypropylene woven bags featuring thick, heat-sealed inner polyethylene liners. For high-volume automated facilities, we offer robust 1000kg flexible intermediate bulk containers (FIBCs) equipped with secure bottom discharge spouts.
Securing a stable caustic soda supply also depends on lightning-fast port connectivity. Situated strategically near major maritime export hubs, our logistics team optimizes FCL container loading up to 28 metric tons per 20ft box, drastically reducing your per-ton ocean freight expenses. Every shipment includes certified Certificates of Analysis (COA) and complete dangerous goods documentation (UN 1823, Class 8) to ensure smooth customs clearance at key African destinations like Lagos, Abidjan, Dakar, Douala, Tema, and Mombasa.


Empower your business with factory-direct pricing, guaranteed monthly volume allocations, and flawless export compliance. Contact our international sales engineering desk today to discuss your annual framework agreements or spot orders, and receive a comprehensive quotation within 24 hours.
Tel:+86-22-66863746
Fax:+86-22-66863746 ext. 608
Mobile Phone:
+86-15822288975(WhatsApp)
E-mail: causticsoda@jiahengyuanchem.com
Add:NO.1023, 10F, BLDG B, JUNJING SQUARE, HANGYUN 1ST ROAD, TEDA, TIANJIN, CHINA