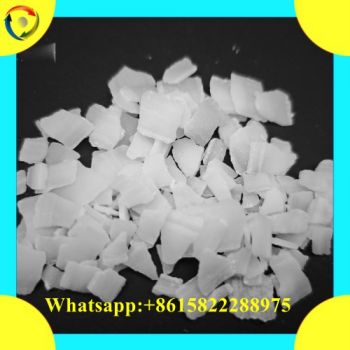
For plant managers, chemical buyers, and industrial distributors across Africa, raw material handling losses and inconsistent dosing can silently drain profit margins. Traditional irregular flakes often create airborne dust hazards during manual feeding and bridge inside automated hoppers, causing costly line stoppages. Sourcing uniform sodium hydroxide pellets (0.8mm to 1.2mm spherical micro-prills) eliminates these operational bottlenecks while delivering rapid, predictable alkalinity for high-volume manufacturing.
By partnering directly with our integrated chlor-alkali production complex, your business bypasses multi-tiered local brokers and secures factory-gate pricing on certified 99.0% minimum purity material. Whether you manage continuous industrial processing lines or distribute bulk chemicals across regional markets, our scalable production capacity guarantees uninterrupted monthly allocations.


Every batch of our spherical alkali undergoes strict quality verification to ensure superior mechanical strength and chemical clarity:
● Free-Flowing Automated Feeding: Calibrated spherical geometry prevents caking and bridging in screw conveyors, volumetric feeders, and automated batching systems.
● Superior Resistance to Tropical Humidity: Compared to flat flakes with larger exposed surface areas, dense spherical pellets exhibit significantly lower moisture absorption rates during warehousing in humid coastal climates.
● Cleaner, Safer Working Environments: High pellet hardness minimizes attrition during transit, virtually eliminating caustic dust clouds when operators open bags on the factory floor.
● Ultra-Low Impurity Profile (NaOH ≥ 99.0%): Strictly controlled sodium carbonate (≤ 0.5%), sodium chloride (≤ 0.03%), and iron content (≤ 0.001%) safeguard sensitive downstream reactions and prevent equipment scaling.

Integrating high-purity sodium hydroxide pellets into your manufacturing workflow enhances product consistency across Africa’s fastest-growing sectors:
1. Commercial Soap and Detergent Manufacturing: Drives rapid, complete saponification of palm, palm kernel, and coconut oils, yielding firm, bright laundry bars with superior lathering performance.
2. Gold Mining and Mineral Processing: Provides exact pH stabilization during cyanide gold leaching, bauxite digestion, and selective flotation of copper and cobalt ores.
3. Beverage Bottling and Dairy Sanitation (CIP): Dissolves cleanly without insoluble sediment for high-efficiency Clean-In-Place sterilization of fermentation tanks, milk lines, and returnable glass bottles.
4. Water Purification and Textile Finishing: Neutralizes acidic industrial wastewater, precipitates heavy metals, and optimizes cotton mercerization for vibrant, uniform dye uptake.

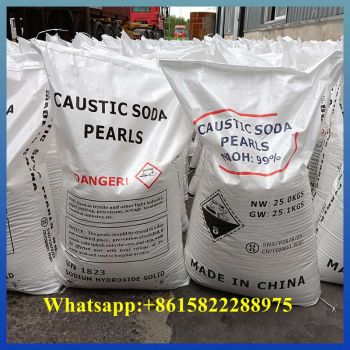
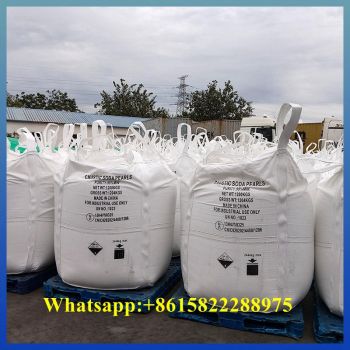
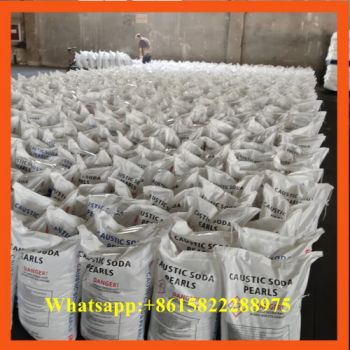
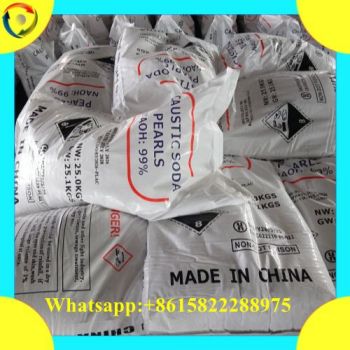
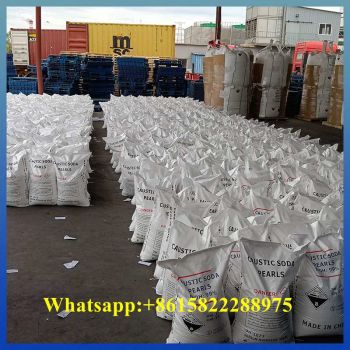
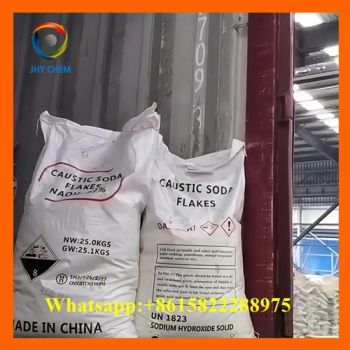
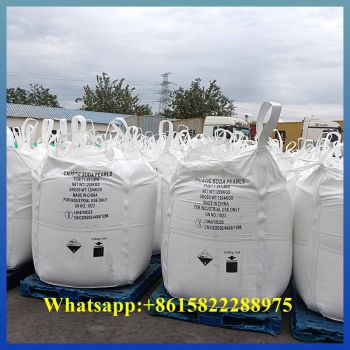
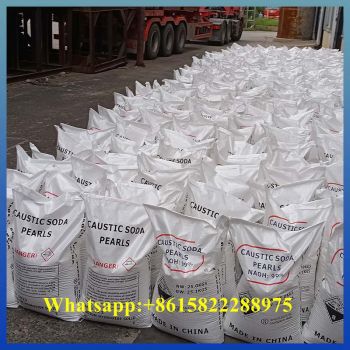
Surviving long maritime voyages to West, East, North, and Southern African ports requires uncompromising packaging engineering. We pack our solid pellets in heavy-duty 25 kg multi-layer woven polypropylene bags lined with thick, heat-sealed virgin polyethylene inner pouches, as well as reinforced 1000 kg jumbo bags fitted with moisture barriers and sturdy lifting straps.
Operating directly alongside major container export terminals, our logistics specialists maximize 20ft FCL container payloads up to 28 metric tons net—substantially lowering your landed freight cost per ton. Every consignment complies fully with IMDG dangerous goods regulations (UN 1823, Class 8) and ships with batch-specific Certificates of Analysis (COA), Safety Data Sheets (SDS), and full support for pre-shipment inspections by SGS or Bureau Veritas to destinations including Lagos, Abidjan, Dakar, Douala, Tema, and Mombasa.
Secure a dependable, cost-effective chemical supply chain built for long-term industrial growth. Contact our international export team today with your required tonnage, packaging preference, and destination port to receive a competitive FOB, CFR, or CIF quotation within 24 hours.
Tel:+86-22-66863746
Fax:+86-22-66863746 ext. 608
Mobile Phone:
+86-15822288975(WhatsApp)
E-mail: causticsoda@jiahengyuanchem.com
Add:NO.1023, 10F, BLDG B, JUNJING SQUARE, HANGYUN 1ST ROAD, TEDA, TIANJIN, CHINA